At
Wolv Engineering, our
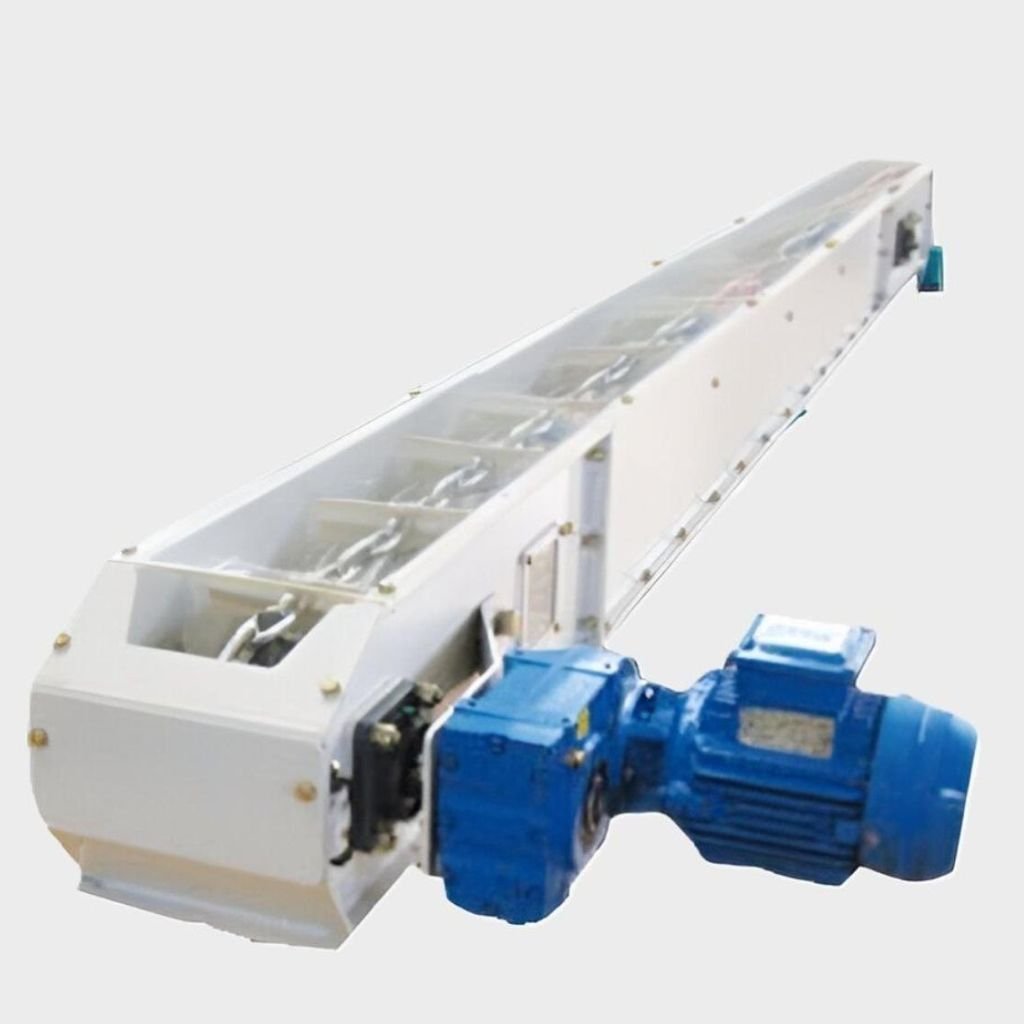
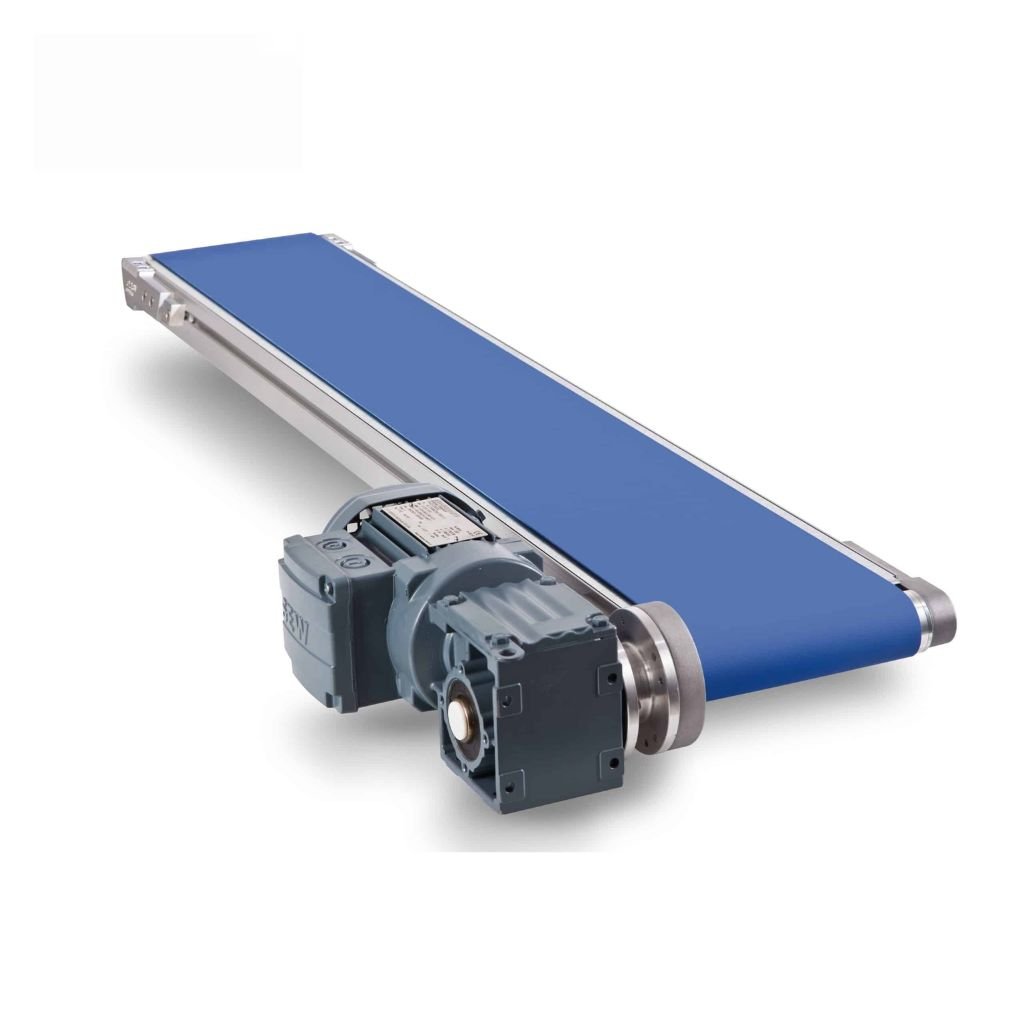
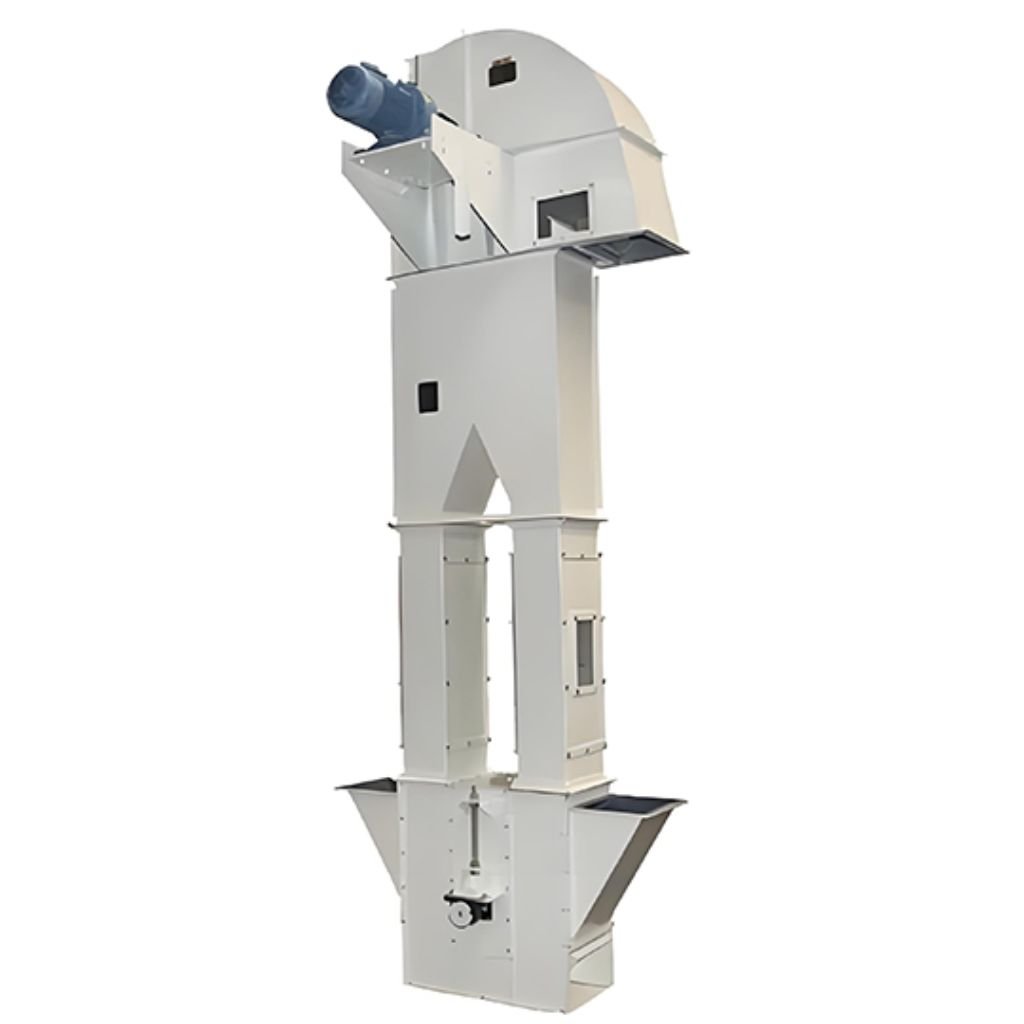
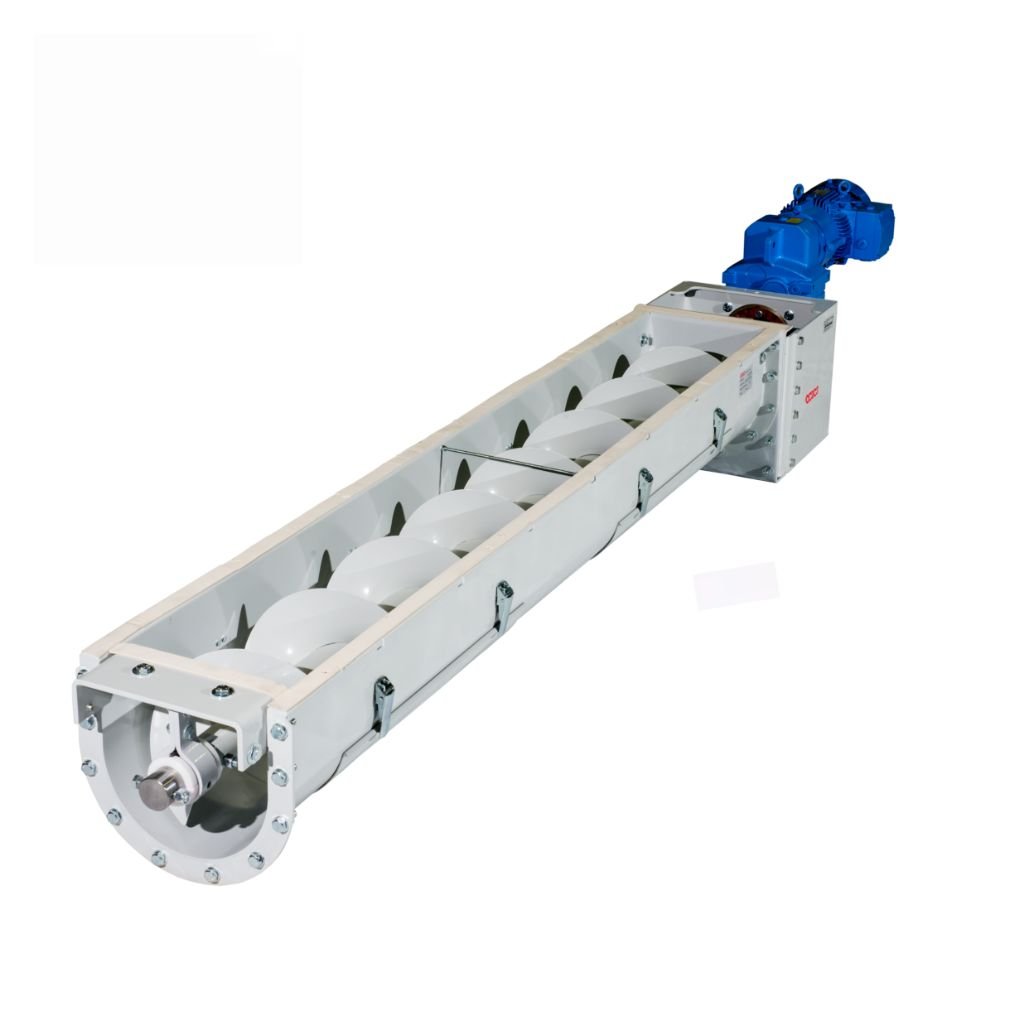
Chain Conveyor Systems are engineered to provide rugged, high-volume mechanical transport for bulk materials. Operating on an “en-masse” drag principle, these systems use high-strength rectangular flights attached to a continuous guided chain loop to smoothly slide material along the bottom of a completely sealed casing. This enclosed design makes them inherently dust-tight, preventing material degradation, eliminating dust hazards, and ensuring an exceptionally hygienic, contamination-free processing environment.
Engineered for Your Industrial Solutions
Our Chain Conveyors serve as a foundational, high-performance link across all major Wolv Engineering Solutions:
-
- Grain Handling & Silo Storage: Ideal for heavy-duty intake lines, horizontal distribution over a series of high-capacity Storage Bins, or material extraction from pits and hoppers.
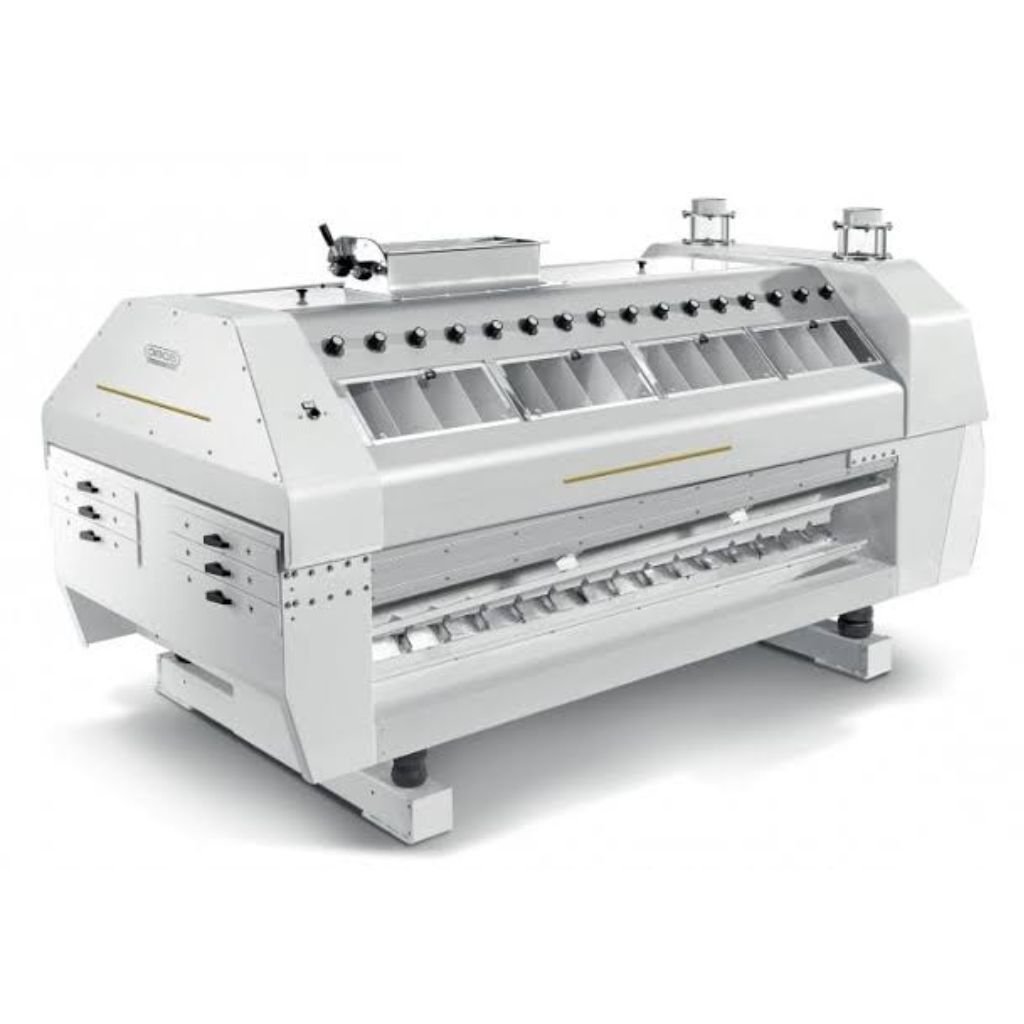
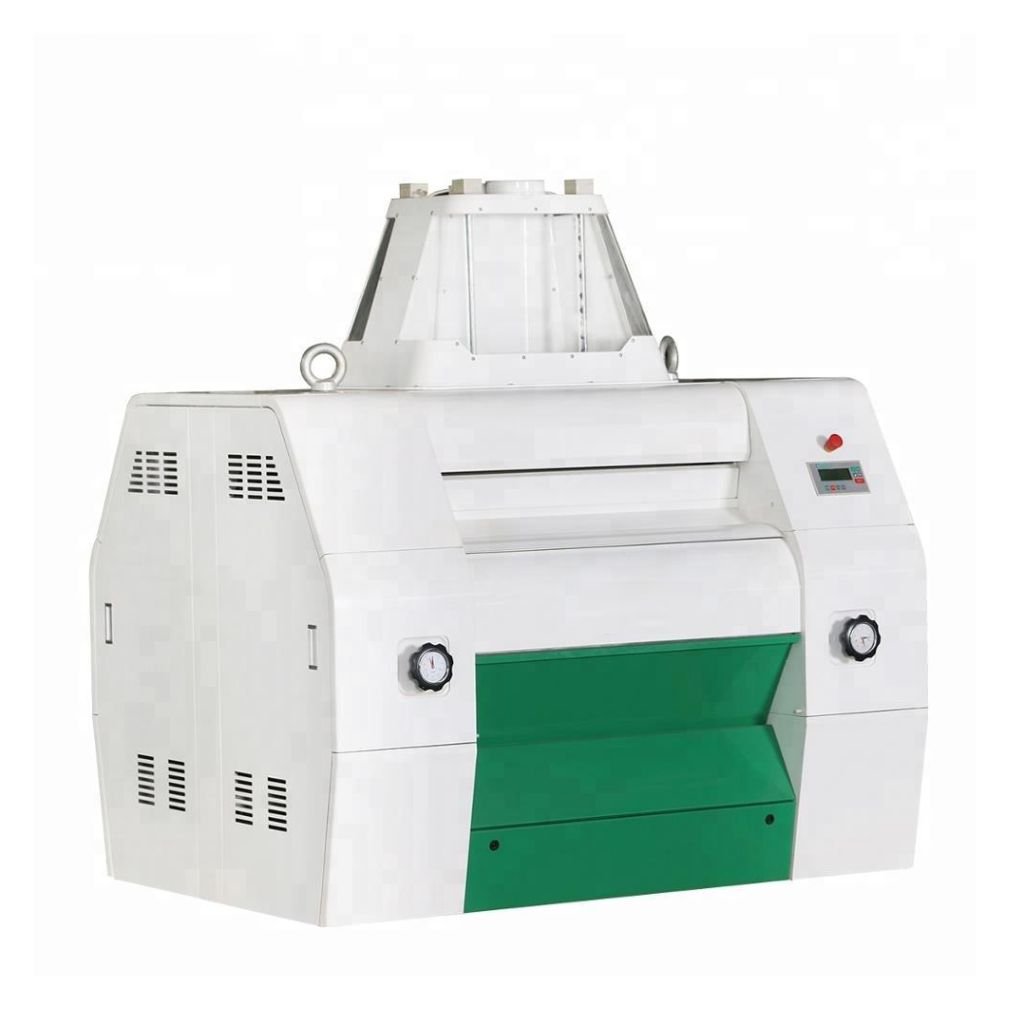
- Flour Milling & Feed Mills: Seamlessly transfers raw or conditioned wheat, barley, corn, and ground ingredients over long distances to reliably feed high-throughput processing lines, matching the pace of your Roller Mills, Hammer Mills, and Plansifters.
- Oil Processing Plants: Ruggedly built with high impact resistance to handle coarse, abrasive, or bulky oilseeds effortlessly before and after the extraction phase.
Our End-to-End Services For Your Chain Conveyor Integration
We provide a comprehensive, single-source engineering approach to your entire conveying line:
- Engineering & Design: Every system is mapped via custom Plant Layouts and Machine Layouts. We optimize material flow through precise chain speed calculation, intermediate multi-point discharge configuration using automated slide valves, and tailored Equipment Sizing to prevent structural bottlenecks.
- Fabrication & Workshop Excellence: Utilizing state-of-the-art CNC Laser Cutting, we manufacture highly rigid, dust-tight casings, wear-resistant bottom liners, and heavy-duty Machine Frames. Our workshop utilizes premium MS & Stainless Steel Fabrication to build rugged head/tail terminals and custom intake Hoppers & Bins built to handle extreme tension and heavy loads.
- On-Site Installation & Commissioning: Our specialized technical team supervises precise mechanical Equipment Alignment (critical for preventing chain twists and sprocket wear), integrates the casings with your building structure and plant Aspiration Systems, and finishes the deployment with comprehensive Trial Operation and Load Testing.